~250 Acres Contract Farming & Raw Material Traceability
Direct farm sourcing eliminates middleman delays, prevents pesticide contamination, and locks in crop freshness before processing.
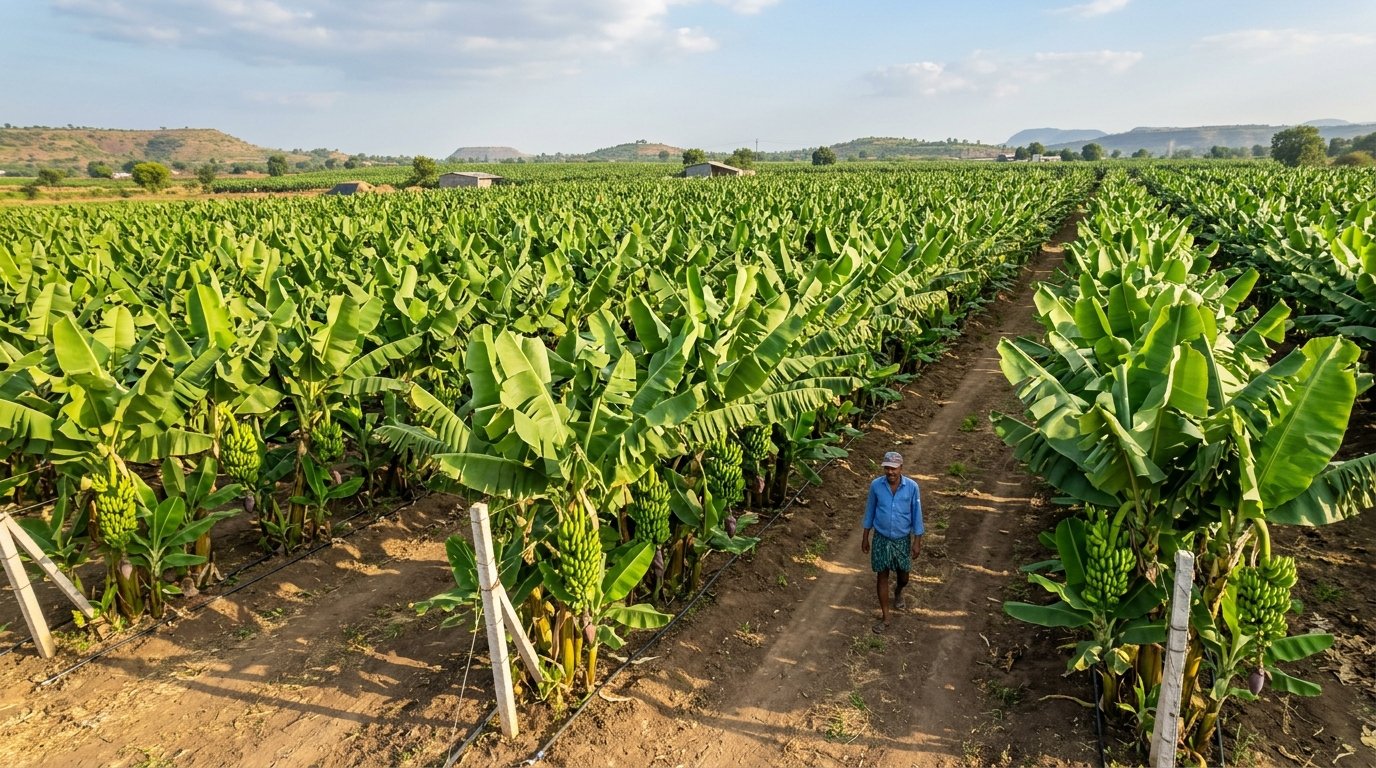
Quality in dehydrated food manufacturing starts long before raw crops arrive at the processing facility. Sourcing 60–70% of our raw materials directly from ~250 acres of contracted farm clusters in Jalgaon allows IMM Food Innovators LLP to enforce strict agricultural discipline, pesticide management, and harvest scheduling.
Strategic Jalgaon Banana Belt Location
Jalgaon is globally recognized as Maharashtra's banana capital. Our facility in Yawal is positioned directly amidst farm clusters, ensuring harvested Grand Naine and Cavendish bananas reach our washing lines in under 4 hours.
Pesticide Control & Soil Testing
Every contracted farm plot undergoes pre-harvest soil and irrigation water testing. We enforce strict pre-harvest interval (PHI) compliance, guaranteeing raw produce is free from harmful chemical residues.
Ethical Farmer Empowerment & Sustainability
We partner directly with local farming families, offering fair pricing contracts, technical guidance on organic farming practices, and crop security—building a resilient, sustainable supply chain.
Low-Temperature Air Dehydration Technology (<45°C - 55°C)
Preserving heat-sensitive bioactives, natural color, original aroma, and dietary fiber without adding synthetic carrier agents or Maltodextrin.
Conventional drying methods like spray-drying subject raw food slurries to extreme thermal shock (160°C to 200°C), degrading heat-sensitive nutrients and requiring up to 30%–50% added Maltodextrin starch fillers. Open solar drying exposes food to dust, humidity variations, and microbial contamination.
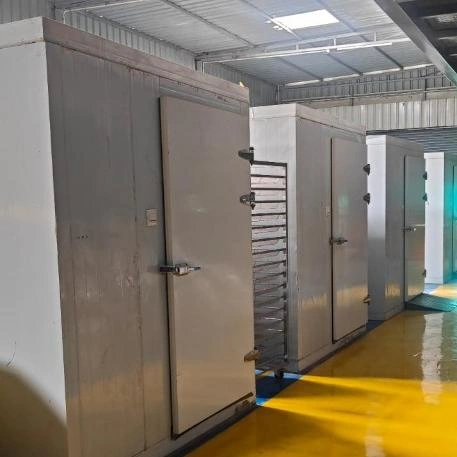
IMM Food Innovators LLP utilizes precision low-temperature hot-air dehydration (<45°C - 55°C) inside clean stainless-steel drying chambers. This gentle thermal process gently extracts moisture while leaving cellular structures and natural bioactives 100% intact.
Zero Maltodextrin, zero dextrose, zero starch additives. Just pure green banana, moringa, or spice solids.
Retains resistant starch (type-2 RS) in raw green raw banana powder, chlorophyll in moringa, and volatile curcumin in turmeric.
Low water activity prevents enzymatic browning and microbial spoilage natively, offering an extended 18–24 month shelf life.
Technical Comparison: Low-Temp Dehydration vs Spray Drying vs Solar Drying
| Parameter / Feature | IMM Low-Temp Dehydration | Conventional Spray Drying | Open-Air Solar Drying |
|---|---|---|---|
| Operating Temperature | <45°C – 55°C (Gentle Heat) | 160°C – 200°C (High Heat) | 35°C – 45°C (Uncontrolled) |
| Carrier Agents / Starch | 0% (100% Pure Ingredient) | 30% – 50% Maltodextrin | 0% (Risk of contamination) |
| Nutrient & Bioactive Retention | 90%–95%+ Preserved | Thermal Degraded (<60%) | UV Degraded (<70%) |
| Hygiene & Microbial Control | Cleanroom Standard (ISO 22000) | Industrial Closed System | High dust & bird risk |
Global B2B Supply & Turnkey Contract Manufacturing
Processing up to 1,000 kg per shift to easily fulfill large commercial contracts, custom recipe blending, and export private labeling.
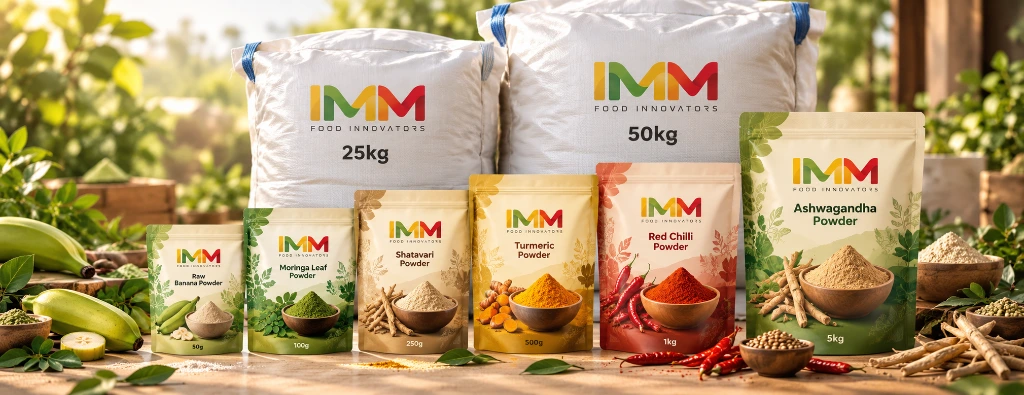
IMM Food Innovators LLP serves as an end-to-end manufacturing partner for food brands, nutraceutical companies, infant food processors, and global ingredient exporters. With processing lines scalable up to 1,000 kg per shift, we provide seamless commercial production with strict batch uniformity.
Custom Particle Sizing (20 to 100+ Mesh)
Equipped with stainless-steel micro-milling machinery capable of producing coarse flakes, granules, or extra-fine 100+ mesh powders for infant formulas and solubility-critical beverages.
Bespoke Spice & Superfood Blending
We offer confidential recipe development and precision homogeneous blending for custom curry powders, herbal wellness teas, ready-to-cook (RTC) seasoning blends, and functional protein mixes.
Lab Evidence Discipline (NABL Accredited)
Every commercial production batch undergoes strict quality testing backed by accredited NABL Certificate of Analysis on file (Shree ATR Lab Jalgaon — TC-14380) for moisture, mesh size, and microbial safety.
Our 6-Step Farm-to-Factory Processing Flow
How our 3 core pillars seamlessly connect to deliver uncompromised purity from Jalgaon farmland to global consumer packaging.
Harvest & Farm Audit
Fresh Cavendish green bananas, moringa leaves, and spices harvested from ~250 contracted farm acres in Jalgaon.
Washing & Sorting
Ozone-purified water washing removes surface debris, followed by manual inspection sorting to ensure only pristine produce enters production.
Low-Temp Dehydration
Gently dried at controlled temperatures (<45°C - 55°C) to lock in natural flavor, vibrant pigments, active enzymes, and dietary fiber.
Hygienic Fine Milling
Stainless steel pulverization and sifting into customized mesh particle sizes (20 mesh to 100+ mesh fine powders) under cleanroom conditions.
NABL Lab Clearance
Batch sample testing at NABL accredited laboratory (Shree ATR Lab Jalgaon — TC-14380) for moisture, microbial, and purity verification.
Moisture-Barrier Dispatch
Sealed into 25kg/50kg HDPE moisture-barrier bulk export drums or custom private-label retail pouches for worldwide shipping.
Certifications & Food Safety Management
IMM Food Innovators LLP operates under international food safety benchmarks and authentic government licenses.

FSSAI Central License
Lic No. 11525073000252

ISO 22000:2018
Food Safety Management

ISO 9001:2015
Quality Management System

GMP Certified
Good Manufacturing Practice

Udyam MSME
Enterprise Registration
Questions About IMM Food Innovators LLP
Got questions about our Jalgaon processing facility, sample testing, or commercial minimum orders?
When was IMM Food Innovators LLP established, and where is the plant located?
IMM Food Innovators LLP was established in 2025. Our state-of-the-art manufacturing plant and corporate facility are located at Nhavi Hambardi Road, at Post Nhavi Pra Yawal, Taluka Yawal, District Jalgaon, Maharashtra - 425524, India.
What makes your dehydrated raw banana powder superior to spray-dried options?
Our low-temperature hot-air dehydration (<45°C - 55°C) preserves natural dietary fiber, essential vitamins, authentic aroma, and resistant starch without adding synthetic carriers like Maltodextrin. Spray drying uses high heat (160°C+) and requires 30–50% added carrier starches.
Can we request accredited lab certificates of analysis (CoA)?
Yes. Every commercial batch undergoes rigorous QA testing. We provide accredited NABL Certificate of Analysis reports from Shree ATR Lab Jalgaon (TC-14380) covering moisture, mesh size, heavy metals, and microbial parameters upon request.
Can prospective B2B clients schedule a tour of your Yawal facility?
We welcome commercial clients, export procurement teams, and brand owners to visit our Yawal manufacturing facility. Contact our sales team at +91 9114403000 or email info@immfoodinnovators.in to schedule an official plant audit.